
Applications
Flue Gas Treatment
SO₂, HCl and HF removal via dry and semi-dry sorbent injection, with sorbent selection and stoichiometry.
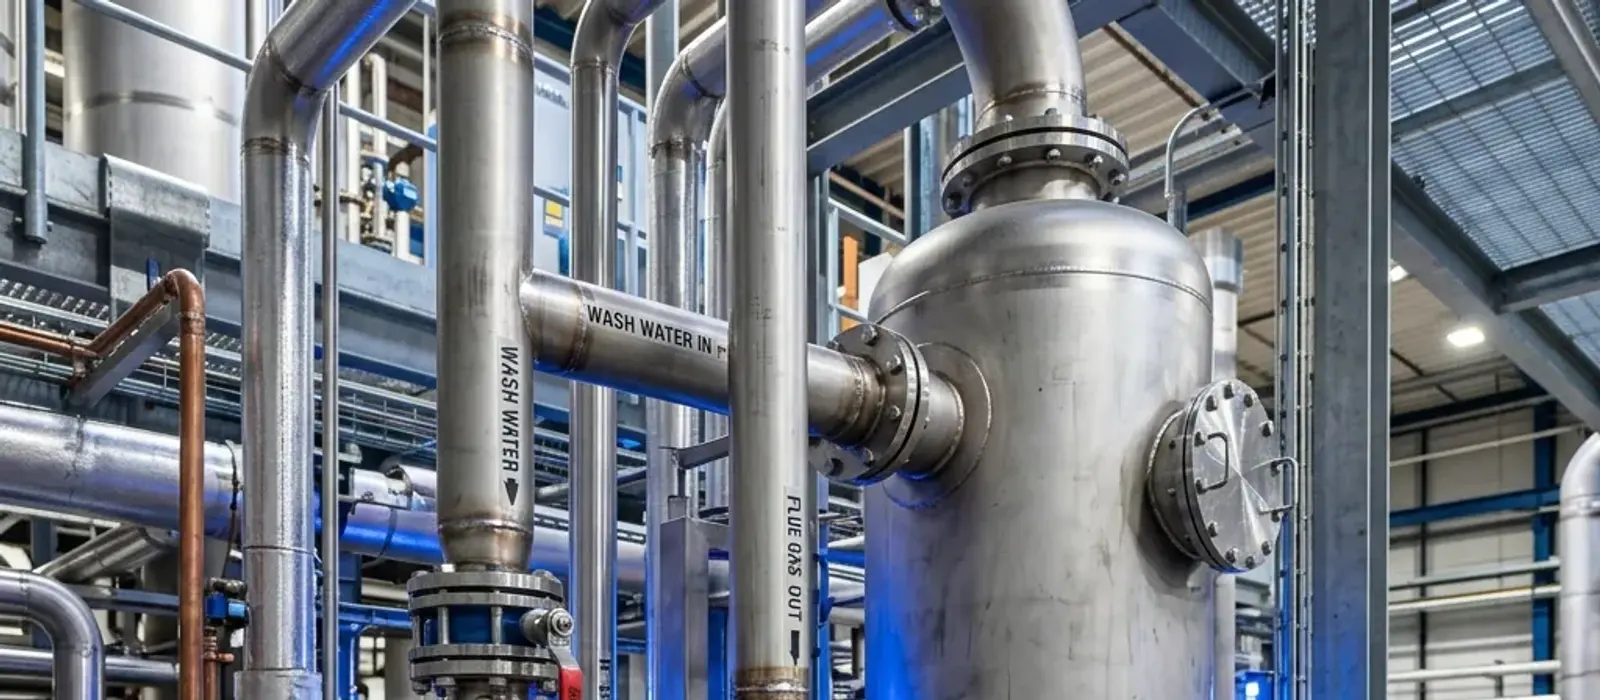
Overview
Flue gas treatment does not solve for one pollutant but for a mixture of acid gases: SO₂ and SO₃ dominate in coal and biomass boilers, HCl and HF dominate in waste incineration, and in glass and ceramic furnaces the two appear together in a shifting ratio. All of them can be captured with a calcium-based sorbent — but not at the same dose, the same fineness or the same temperature window.
Dry and semi-dry sorbent injection has become the dominant route for mid-sized plants because it produces no wastewater, costs less to install and does not require reheating the flue gas. The real engineering problem here is not chemical but one of contact: the reaction between a hydrated lime particle and a gas molecule runs only on the outer surface and in the open pores of that particle, and is expected to finish within seconds.
That is why chemical purity of the sorbent comes second in a flue gas line; what decides the outcome is BET surface area, pore volume and particle size distribution. VisneChem approaches this field by treating sorbent properties, the Ca/S stoichiometric ratio and the approach temperature as a single operating window. Changing one of these three independently of the others usually raises consumption without cutting emissions as much as expected.
Where the solid–gas reaction actually stops
When a Ca(OH)₂ particle meets SO₂ it forms a surface layer of CaSO₃·½H₂O; with HCl it forms a calcium-chloride salt layer. The molar volume of this product layer is larger than that of the reactant, so it closes the pore mouths and stops gas diffusion into the particle core. The consequence: a large share of the calcium fed into the duct reaches the filter ash without ever reacting. That is not poor operation but the natural outcome of the reaction mechanism; the goal is not 100% conversion but the required removal at an acceptable Ca/S ratio.
The second limit is residence time. In-duct contact is typically 1–3 seconds; at a gas velocity of 15–20 m/s that means only 20–50 metres between the injection point and the filter. Full conversion is impossible in that time. Most of the actual removal — 50–80% in most plants — happens in the cake built up on the bag filter, where contact time rises to the order of minutes. Filter cleaning interval, air-to-cloth ratio and cake thickness are therefore chemical parameters, not merely dust-collection parameters.
Temperature squeezes the window from both ends. In dry injection Ca(OH)₂ dehydrates back to CaO above roughly 400 °C and loses reactivity as its pore structure collapses; below 140 °C, SO₃ and water vapour approach the acid dew point and corrosion starts in the duct and the filter. In semi-dry systems what matters is not absolute temperature but the approach to adiabatic saturation temperature (ΔT). The usual working band is 15–30 K: the narrower ΔT gets, the higher the removal — and the higher the risk of sticking, agglomeration and pressure drop on the bags.
The most misleading figure is the Ca(OH)₂ percentage on the sorbent certificate. Two hydrated limes may both assay 94%; if one has a BET surface of 16 m²/g and the other 38 m²/g, the dose needed for the same removal differs by nearly a factor of two. The second trap is the reference condition of the emission value: unless the SO₂ result is on a dry basis and corrected to the right O₂ reference (6% for coal firing, 11% for waste incineration), dilution air leaking into the system flatters the number on its own. An analyser without QAL3 drift control under EN 14181 slides quietly over months, and the dose is then tuned against that drifted number.
Which sorbent, at what fineness, at what temperature
The standard material for dry sorbent injection is hydrated lime (Ca(OH)₂, typically class CL 90-S to EN 459-1). It is conveyed pneumatically from the silo and injected straight into the duct; no water line, slurry pump, agitator or effluent treatment is needed. With a standard hydrate the typical Ca/S molar ratio for 85–95% SO₂ removal is 1.8–3.0. The way to lower that ratio is not more lime but better surface.
A high-surface hydrate (BET 30–45 m²/g, pore volume 0.15–0.20 cm³/g) delivers the same removal at Ca/S 1.3–1.8. Its price per tonne is above standard hydrate, but because consumption falls, both total reagent spend and the volume of residue to be disposed of go down. The right decision comes from the sum of lime price and residue disposal cost; comparing tonne prices alone leads most plants to the wrong answer.
In a semi-dry spray dryer absorber (SDA) the sorbent is fed as milk of lime. Producing that slurry on site from quicklime is cheaper per mole of Ca than buying ready hydrate; but the particle size and surface area of the Ca(OH)₂ the slaker produces depend entirely on slaking conditions. Unless slaking water temperature, water-to-lime ratio and CaO reactivity (the t₆₀ test in EN 459-2) are controlled, the same feedstock yields slurry of widely varying quality and dosing becomes unstable.
In circulating fluidised bed boilers the sorbent goes straight into the bed as natural calcium carbonate. Here the calcination window is narrow: at 820–870 °C CaCO₃ decomposes and releases porous CaO; above 900 °C sintering closes the pores and the Ca/S ratio climbs quickly. The same feedstock also serves wet scrubbers, but there the governing parameters are dissolution rate and impurity level — MgO and acid-insoluble residue in particular — rather than surface area.
Fineness is the parameter common to both routes: dry injection targets D50 of 4–8 µm and D97 below 40 µm. The fraction above 40 µm practically never reacts; it only adds filter load and residue volume. Particle size is measured by laser diffraction to ISO 13320 and surface area by BET to ISO 9277 — without those two numbers two sorbents cannot be compared. Because unreacted free lime in the filter ash is typically 40–60%, recycling that ash cuts fresh sorbent consumption by 20–40%, a practice also common on sinter plant and electric arc furnace lines.
Operating ranges
| Parameter | Value | |
|---|---|---|
| Ca/S molar ratio — dry, standard hydrate | 1.8–3.0 | For 85–95% SO₂ removal |
| Ca/S molar ratio — high-surface hydrate | 1.3–1.8 | BET ≥ 30 m²/g |
| Ca/S molar ratio — semi-dry (SDA/CDS) | 1.1–1.6 | Milk of lime or humidified hydrate |
| Ca/(Cl+F) molar ratio | 1.1–1.6 | HCl and HF; faster reaction than SO₂ |
| Dry injection temperature | 140–350 °C | Lower limit acid dew point, upper limit dehydration |
| Approach to saturation (ΔT) | 15–30 K | Semi-dry; narrow ΔT means bag blinding |
| Sorbent fineness D50 / D97 | 4–8 µm / < 40 µm | ISO 13320, laser diffraction |
| BET surface area | 15–20 / 30–45 m²/g | Standard / high reactivity; pore volume 0.08–0.20 cm³/g, ISO 9277 |
| In-duct residence time | 1–3 s | 20–50 m at 15–20 m/s gas velocity |
| Bag filter air-to-cloth ratio | 0.8–1.2 m/min | To preserve the cake-reactor effect |
| Ash recirculation ratio | 3–10 × | Free lime in ash 40–60% |
| Emission reference condition | dry gas, 6% / 11% O₂ | Coal / waste incineration; EN 14791, EN 1911 |
Ca/S molar ratio — dry, standard hydrate
1.8–3.0
For 85–95% SO₂ removal
Ca/S molar ratio — high-surface hydrate
1.3–1.8
BET ≥ 30 m²/g
Ca/S molar ratio — semi-dry (SDA/CDS)
1.1–1.6
Milk of lime or humidified hydrate
Ca/(Cl+F) molar ratio
1.1–1.6
HCl and HF; faster reaction than SO₂
Dry injection temperature
140–350 °C
Lower limit acid dew point, upper limit dehydration
Approach to saturation (ΔT)
15–30 K
Semi-dry; narrow ΔT means bag blinding
Sorbent fineness D50 / D97
4–8 µm / < 40 µm
ISO 13320, laser diffraction
BET surface area
15–20 / 30–45 m²/g
Standard / high reactivity; pore volume 0.08–0.20 cm³/g, ISO 9277
In-duct residence time
1–3 s
20–50 m at 15–20 m/s gas velocity
Bag filter air-to-cloth ratio
0.8–1.2 m/min
To preserve the cake-reactor effect
Ash recirculation ratio
3–10 ×
Free lime in ash 40–60%
Emission reference condition
dry gas, 6% / 11% O₂
Coal / waste incineration; EN 14791, EN 1911
Application steps
- 01
Mapping the flue gas and the load profile
SO₂, SO₃, HCl, HF, dust, moisture, O₂ and temperature are measured simultaneously. An average is not enough to size the system; the peak load decides it. In waste incineration and plastics recycling lines a change of feed batch can triple the HCl load within ten minutes, and in coal-fired boilers sulphur content shifts with seam and supplier.
SO₃ must be measured by its own method (controlled condensation); a standard SO₂ analyser does not see it, yet SO₃ drives a large part of both sorbent consumption and the acid dew point. The measurement plane must satisfy the homogeneity and access requirements of EN 15259 — where the pollutant distribution across the cross-section is uneven, a single-point value misdirects the entire design.
- 02
Sorbent selection and laboratory reactivity testing
Candidate sorbents are characterised by BET surface area (ISO 9277), pore volume, particle size distribution (ISO 13320), free moisture and degree of carbonation. Comparison must always be made at equal Ca/acid molar ratio, never at equal mass; comparing two products of different purity on a kilogram basis corrupts the result at the outset.
Reactivity testing must use a composition close to the real flue gas: HCl, water vapour and O₂ alongside SO₂. A ranking obtained in dry synthetic gas does not reproduce in the field, because water vapour both accelerates the surface reaction and alters the structure of the product layer. The curve from a fixed-bed or entrained-flow reactor gives the first estimate of the plant's Ca/S window.
- 03
Injection point and distribution design
The number, angle and cross-sectional placement of injection lances decide how quickly the sorbent disperses into the gas stream. Gas velocity is typically held between 12 and 20 m/s; the distance from injection point to filter translates directly into residence time. Jet dispersion is verified by CFD — injection close to the wall produces floor deposits and eventual blockage.
Carrier air flow and pressure are critical for dispersing the sorbent without agglomeration. Hydrate that has picked up moisture bridges in the silo and feeds unevenly through the dosing screw, showing up as minutes-long spikes on the emission trace. Silo, aeration, dosing screw and eductor must be designed as one feed chain rather than as separate items of equipment.
- 04
Humidity and approach temperature control
In semi-dry systems, water injection is set to hold the gas 15–30 K above adiabatic saturation temperature. Each droplet must evaporate fully within its flight time in the duct; a droplet that does not evaporate creates wet deposits on the duct floor, corrosion and eventually hard build-up. Nozzle selection and atomising pressure are therefore part of chemical performance.
Duct humidification also lifts removal markedly in dry systems (conditioned dry injection); a gain of 10–20 percentage points at the same Ca/S is common. But once the dew point margin falls below 15–20 K, bag blinding and duct corrosion begin. Temperature must be tracked separately at the filter inlet and outlet, not managed from a single point.
- 05
Bag filter and cake management
In this process the bag filter is not only a dust collector but a second reactor. The air-to-cloth ratio is held between 0.8 and 1.2 m/min and pressure drop typically between 1000 and 2000 Pa. The longer the cleaning interval, the longer the residence in the cake and the higher the removal; stretched too far, the price is pressure drop, fan energy and bag fatigue. The optimum is a deliberate choice between emission and energy.
Bag material is chosen for temperature and chemical environment: PPS up to roughly 190 °C continuous, PTFE to around 250 °C, PTFE-membrane glass fibre higher still. In semi-dry operation the humidity margin sets the fabric's hydrolysis resistance; PPS ages faster than expected where high O₂ and moisture coincide. Bag life and sorbent choice are coupled at exactly this point.
- 06
Recirculation and cutting sorbent consumption
Unreacted free lime in the filter ash is measured (sugar or EDTA methods under ASTM C25). If it falls in the 40–60% band, recirculation makes economic sense. Returning the ash to the injection line at 3–10 times the fresh rate typically cuts fresh sorbent consumption by 20–40% and reduces the residue for disposal in the same proportion.
Lightly humidifying the recycled ash cracks the product layer and partly reopens closed pores; the effect is clear on the removal curve. But if moisture goes too high, sticking and blockage start in the ash handling lines — 2–5% is the safe band on most plants. The recycle ratio is not a fixed number but a setting updated periodically against free-lime analysis of the ash.
- 07
Measurement, calibration and the dosing control loop
The continuous emission monitoring system is managed under EN 14181: QAL1 suitability, QAL2 calibration and QAL3 ongoing drift control. QAL2 calibration uses the standard reference methods — EN 14791 for SO₂, EN 1911 for HCl, EN 13284-1 for dust. Skip QAL3 and the analyser drifts within months, after which dosing is tuned against an emission value that does not exist.
A control loop watching only stack SO₂ is always late; the lag through the filter cake is minutes long and a load spike has passed before feedback responds. The right architecture combines feed-forward from the inlet load with feedback from the outlet. That lowers average consumption and prevents half-hourly average exceedances at the same time.
- 08
Residue management and commissioning
The residue is a mixture of CaSO₃/CaSO₄ and chloride salts, unreacted Ca(OH)₂ and fly ash. Calcium chloride is hygroscopic and highly water-soluble, which governs how the residue stores, handles and leaches. In waste incineration this residue is usually classified as hazardous waste and requires stabilisation — disposal cost is an inseparable part of the sorbent decision.
During commissioning the Ca/S ratio is raised step by step to trace the removal curve and see where it plateaus. The aim is to operate in the middle of the BAT-AEL band, not just beneath the permit limit, so that load swings still have margin. For a plant-specific sorbent specification, Ca/S window and recirculation strategy you can work through it with our technical team.
Products used in this field



Frequently asked questions
How do I choose between dry sorbent injection and a semi-dry system?
The deciding factors are the inlet acid gas load and the removal target. For targets below 90% and moderate SO₂ load, dry injection is usually sufficient and the plant is far simpler. Where 95% or higher removal meets a high load, a semi-dry system brings Ca/S down to 1.1–1.6 and repays itself on reagent cost over time.
Why is the Ca/S ratio around 2 rather than the stoichiometric 1.0?
Because the reaction runs only at the particle surface. The CaSO₃/CaSO₄ layer that forms closes the pore mouths and blocks gas access to the core. With only 1–3 seconds of in-duct contact, conversion never completes; practical conversion with a standard hydrate sits in the 35–55% band.
Should I use hydrated lime or quicklime?
For dry injection the answer is clear: hydrated lime, because it goes straight into the duct with no water line. Quicklime only makes sense on semi-dry (SDA) lines where milk of lime is prepared; there it lowers cost per mole of Ca, but if slaking conditions are not controlled the slurry quality and the dose both become unstable.
Does a high-surface hydrate justify its extra cost?
On most plants yes, but the decision must be made on total cost, not tonne price. Moving from Ca/S 2.5 to 1.5 cuts consumption by roughly 40%, and cuts the residue for disposal by the same 40%. Where the residue is classified as hazardous waste, that second saving usually outweighs the price difference on the lime.
Are HCl and HF easier to remove than SO₂?
Yes, distinctly. HCl reacts with Ca(OH)₂ faster than SO₂ does, and the product layer obstructs diffusion less. The Ca/(Cl+F) ratio therefore stays in a near-stoichiometric band of 1.1–1.6. In waste incineration the dose is usually set by SO₂, with HCl removed as a by-product of that dose.
Why is the injection temperature window so narrow?
The upper limit comes from dehydration of Ca(OH)₂: above roughly 400 °C it converts to CaO and loses reactivity as its pore structure collapses. The lower limit is the acid dew point; below about 140 °C, SO₃ and water vapour condense and start corrosion in the duct and filter. The operating band lies between those two.
How much does sorbent fineness matter?
As much as surface area, because together they define the area open to reaction. Once D97 exceeds 40 µm, that coarse fraction practically never reacts; it only adds filter load and residue volume. Asking a supplier for a full particle size curve measured to ISO 13320 tells you far more than a single D50 figure.
Does recycling filter ash really cut consumption?
Yes, if free lime in the ash is in the 40–60% band. A recycle ratio of 3–10 typically cuts fresh sorbent consumption by 20–40%. Light humidification of the ash (2–5%) cracks the product layer and strengthens the effect, but too much moisture starts sticking and blockage in the ash handling lines.
Can limestone (CaCO₃) be injected directly into the duct?
Not at duct temperatures — calcination needs above 800 °C, and the duct never reaches it. Limestone belongs in in-bed injection (CFB boilers, 820–870 °C) and in wet scrubbers. For dry in-duct injection the calcium source must be Ca(OH)₂.
A dry system produces no wastewater — but what happens to the residue?
It leaves as a dry solid: sulphite/sulphate, chloride salts, unreacted lime and fly ash. In waste incineration it is usually classified as hazardous waste and needs stabilisation. A wet scrubber shrinks that line item but then requires a separate wastewater treatment train for the blowdown; the comparison must be made with both costs in view.
Sample and dose recommendation for this process
Describe your current usage and target; our technical team will come back with a suitable specification and a starting dose.